
Application Case: Salt-Alkali Chemical
Project Background
At an ink production base, the factory manufactures inks, paints, and coatings using powdered raw materials such as carbon black, with a daily capacity of approximately 20 tons. Although the facility previously utilized sealed feeding rooms with manual labor, the significant pollution and health hazards associated with powder handling became increasingly prominent.
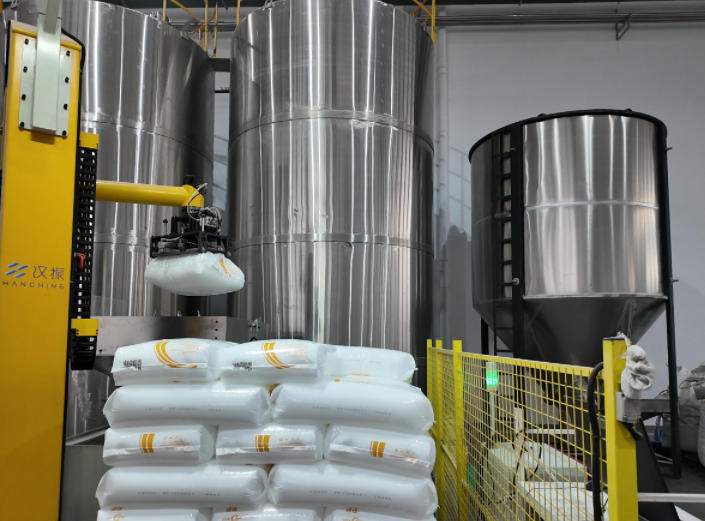
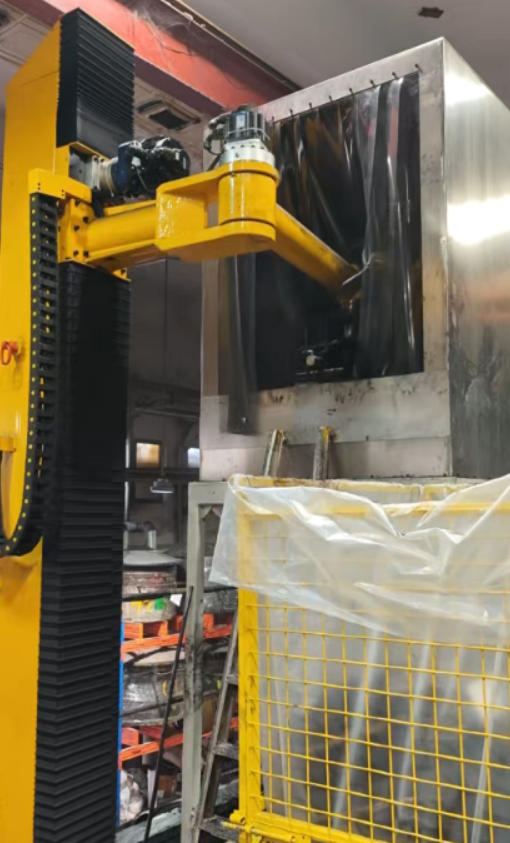
The project faced key challenges: the client used diverse packaging types—including kraft paper bags and PE bags—requiring greater equipment compatibility, while traditional bag-shaking feeding generated substantial dust that needed optimization.
To address this, the project deployed Hanchine's Lite Series standard machines, optimizing the gripper to handle wider kraft paper bags and upgrading the cutting tool to a powered disc cutter for easier opening of rigid bags. Finally, integrating the system with the client’s negative-pressure dust hood at the discharge hopper effectively resolved workshop dust pollution issues.
Challenges
Occupational Health Risks
Powder materials (e.g., carbon black) pose significant health hazards, making manual feeding increasingly unsustainable.
Packaging Diversity
A wide variety of bag types (kraft paper, PE) demanded higher compatibility from the equipment.
Dust Control Difficulty
Traditional feeding methods generated excessive dust, failing to meet clean production standards.
Solution
Base Machine
Deployment of Hanchine's Lite Series Standard Machine.
Targeted Optimization
Gripper optimized for wide kraft paper bags; cutting tool upgraded to a powered disc cutter for rigid packaging.
System Integration
Coordination with the client’s existing negative-pressure dust hood system at the hopper.
Application Value
Health & Safety
Replacing manual labor eliminates human exposure to hazardous powders, improving the working environment.
High Compatibility
Successfully solved the universal handling challenge for mixed packaging types.
Environmental Compliance
Effective dust control met stringent environmental and safety standards for the chemical industry.
rOI
Doubled Efficiency
Robotic high‑speed bag opening with stable cycle time and significant capacity increase.
Labor Reduction
Cuts 2–3 operators per line, reducing labor costs by ~60%.
Near‑Zero Residuals
High‑precision feeding minimizes leftover material and maximizes raw material utilization.